Introduction
The life sciences industry requires precise process control, consistent product quality, and reliable manufacturing operations. Pharmaceutical and biotechnology manufacturers must maintain controlled production environments while adapting to evolving regulatory requirements and technological advancements.
However, outdated automation systems, limited process visibility, and obsolete equipment can affect productivity and operational reliability.
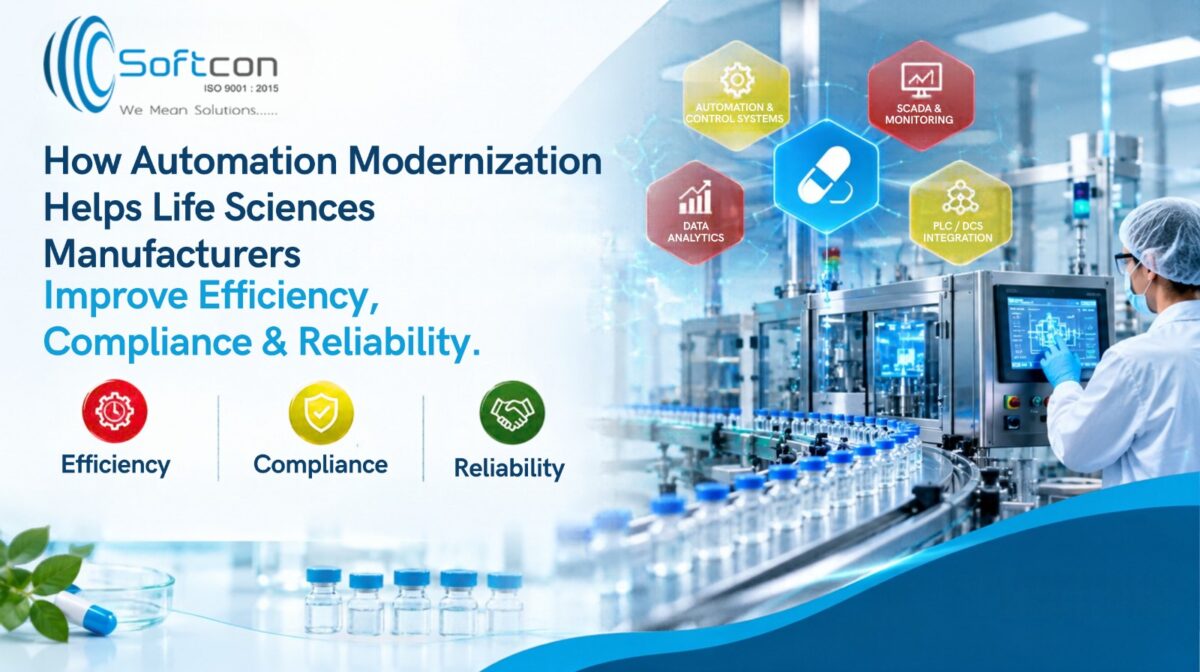
Automation modernization in life sciences manufacturing helps address these challenges by upgrading legacy control systems, improving industrial connectivity, and enabling better access to real-time process data. These improvements help manufacturers build a more efficient, reliable, and scalable production environment.
1. Improving Manufacturing Efficiency Through Automation
Manufacturing efficiency is essential for pharmaceutical companies looking to optimize production and reduce operational interruptions.
Modern automation systems help streamline manufacturing processes by improving communication between controllers, sensors, equipment, and supervisory applications.
Upgraded PLC, DCS, and HMI systems enable better process monitoring, automated control, and faster fault identification. Real-time visibility allows operators to identify deviations and respond to changing process conditions more effectively.
By reducing unnecessary manual intervention and improving process consistency, automation modernization can support improved production performance.
2. Supporting Regulatory Compliance and Data Integrity
Regulatory compliance is a critical requirement in pharmaceutical manufacturing. Companies must maintain accurate records, controlled processes, and traceable manufacturing activities.
Modern automation systems can support these requirements through electronic records, audit trails, process monitoring, and controlled user access.
Depending on the application, automation systems may need to support applicable Good Manufacturing Practice (GMP) requirements and FDA 21 CFR Part 11 for electronic records and electronic signatures.
However, technology upgrades alone do not guarantee compliance. Systems must be appropriately designed, tested, validated where required, and maintained within the manufacturer’s quality management framework.
3. Modernizing Legacy PLC, DCS, and SCADA Systems
Many manufacturing facilities continue to depend on legacy automation infrastructure that may face hardware obsolescence, limited vendor support, and compatibility challenges.
PLC modernization can improve controller performance and diagnostics, while DCS modernization can strengthen process control and system maintainability.
Similarly, SCADA and HMI upgrades can provide clearer process visualization, improved alarm management, and better access to historical trends.
A phased modernization strategy allows manufacturers to prioritize critical systems, assess compatibility, and plan upgrades while minimizing production disruption.
This approach also creates opportunities to integrate existing equipment with newer industrial technologies without necessarily replacing the entire automation infrastructure.
4. Enhancing Process Reliability and Equipment Availability
Reliable automation systems are essential for maintaining manufacturing continuity. Equipment failures, communication interruptions, and limited diagnostic information can lead to unplanned downtime.
Modern control systems provide improved diagnostics, fault monitoring, and support for redundancy in critical applications.
Industrial network monitoring and appropriate controller redundancy can help improve system availability, depending on the architecture and implementation.
By identifying potential issues more effectively, maintenance teams can troubleshoot problems faster and plan maintenance activities with greater confidence.
5. Enabling Real-Time Monitoring and Data-Driven Decisions
Modern manufacturing environments generate significant amounts of process and equipment data. However, this data creates value only when it is accessible, reliable, and useful for operational decisions.
Integrating PLC, DCS, SCADA, HMI, and industrial data platforms can help manufacturers monitor process parameters, review historical trends, and investigate recurring deviations.
Where appropriate, integration with Manufacturing Execution Systems (MES) and enterprise applications can improve information exchange between production and business operations.
These capabilities support better process visibility and provide a foundation for advanced analytics, predictive maintenance, and future digital transformation initiatives.
6. Key Considerations Before Modernizing Automation Systems
Successful automation modernization requires careful planning and an understanding of existing manufacturing requirements.
Manufacturers should evaluate:
- System obsolescence: Availability of spare parts, software support, and engineering resources.
- Regulatory requirements: Impact on validated systems, electronic records, and documentation.
- System integration: Compatibility with existing equipment and applications.
- Cybersecurity: Network segmentation, access controls, and protection of operational technology.
- Production continuity: Migration planning, testing, backups, and recovery procedures.
- Future scalability: Ability to support additional equipment, production lines, and changing requirements.
A structured approach helps manufacturers prioritize investments while managing technical risks and operational constraints.
How Softcon Supports Industrial Automation Modernization
Softcon Systems provides industrial automation and control solutions involving PLC, DCS, SCADA, HMI, industrial networking, and process monitoring.
Our automation expertise supports initiatives focused on improving system connectivity, process visibility, and operational reliability.
For life sciences manufacturers, a well-planned modernization strategy can help address legacy system challenges, improve access to process information, and create a more maintainable automation infrastructure.
Every project should be evaluated according to its technical requirements, production environment, and applicable compliance obligations.
Conclusion
Automation modernization is an important step for life sciences manufacturers seeking to improve efficiency, maintain reliable operations, and address the limitations of legacy control systems.
By upgrading PLC, DCS, and SCADA platforms, strengthening industrial connectivity, and improving process data visibility, manufacturers can build a more scalable and maintainable production environment.
A successful modernization strategy combines appropriate technology, careful migration planning, effective cybersecurity, and consideration of applicable regulatory requirements.
Ready to modernize your automation?
Modernize your automation. Strengthen reliability. Enable better manufacturing.
Talk to Softcon Systems about an automation assessment for your facility. Contact our team to discuss your current systems and upgrade priorities.